If you’re reading this, chances are you’re either on the production floor of a telecom infrastructure company, managing a team that operates PE microduct bundle pipe COD pipe machines, or maybe you’re the person who fields the 2 a.m. calls when the line goes down and a critical order is due. I’ve been on all those sides—first as a production supervisor troubleshooting a stubborn machine that was losing 20% of its weekly output, and now as someone on the supplier side, working directly with operators, maintenance teams, and plant managers to refine how these machines run. Today, I want to pull back the curtain on the small, often overlooked adjustments that add up to big gains in production efficiency for these specific machines. This isn’t about flashy overhauls; it’s about workable, data-backed changes that you can implement next week, without blowing your maintenance budget. PE Microduct Bundle Pipe COD Pipe Machine
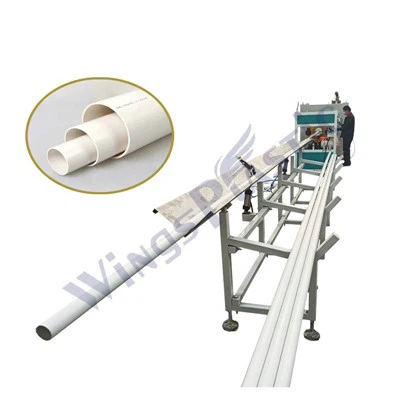
Let’s start with a foundational fact I learned the hard way: PE microduct bundle pipe COD pipe machines have a lot of moving parts, but the biggest bottleneck almost never comes from the extruder itself. Early in my career, I spent months upgrading a single extruder to run at a higher temperature, only to realize the take-up unit was slowing the entire line down. For those who don’t work with these machines daily, a COD pipe (central office duct) bundle is a multi-channel PE pipe used to house fiber optic cables, usually made with 2 to 12 individual microducts bound together. The machine that makes it combines melted PE resin, shapes the individual ducts, binds them into a bundle, and cools it before it’s cut to length. The line’s speed is only as fast as its slowest component, and most plants miss that mark because they’re not auditing each stage of the line individually.
The first actionable step I now recommend to every client is to conduct a “line audit” during a live production run, not a test run. Test runs often use perfect, pre-dried resin and zero downtime, so they don’t reflect real conditions. For a full 8-hour shift, log the speed of each key component every 30 minutes: the extruder output, the calibrator that sets the pipe’s inner and outer diameter, the cooling trough, the binder that holds the bundle together, and the take-up unit. I worked with a mid-sized telecom component manufacturer last year that did this audit and found their take-up unit was set to a fixed speed, but the extruder was ramping up slightly every hour. The take-up couldn’t keep up, so the line would jam, creating a 15-minute delay each time. Once they adjusted the take-up to sync with the extruder’s variable frequency drive (VFD), their downtime from jams dropped by 18% in the first month. That’s not a small number—18% of a full shift is almost a full extra production block, enough to cut one order lead time by three days.
Next, let’s talk about resin preparation, a step that’s surprisingly tied to machine efficiency. Most PE resins used for COD pipes are hygroscopic, meaning they absorb moisture from the air. If resin isn’t properly dried before it goes into the extruder, you get what operators call “silver streaks”—tiny bubbles or discolorations that force a full line shutdown to fix, or worse, a batch of scrap pipe that has to be reworked. I’ve seen plants use old, under-sized dryers that take 4 hours to reach the required drying temperature (160°F to 180°F for standard PE) and leave residual moisture. The fix here isn’t just buying a bigger dryer, either—it’s matching the dryer’s capacity to the machine’s extruder output, and adding a desiccant bed maintenance step. One client was using a 50-lb dryer for an extruder that ran at 200 lbs per hour; the dryer could never keep up, so resin had to sit in a holding bin before extrusion, which meant it absorbed moisture again. Swapping to a 200-lb desiccant dryer with a daily bed purging cycle cut scrap from moisture-related issues by 92% in two months. That’s less time throwing away good material and restarting the line, which translates directly to more running time.
Calibration is another area where small adjustments make a huge difference. The calibrator is the component that shapes the hot molten PE into the exact inner and outer diameter required for the microducts. If the calibrator is misaligned by even 0.1mm, the pipe doesn’t pass through the cooling trough evenly, leading to warping that causes jams in the take-up unit or binding issues. Most operators calibrate the machine when they first set up a new batch, but they don’t check it again for weeks. I suggest a weekly calibrator alignment check, using a digital micrometer to measure the pipe’s diameter at three points along the line, and adjusting the calibrator’s tension screws if there’s more than a 0.05mm variance. I also advise upgrading from a manual calibrator to a pneumatic calibrator, which uses air pressure to hold the pipe in place instead of manual tension. This eliminates human error in calibration, and one client saw their line uptime jump by 12% after making the switch. Pneumatic calibrators aren’t cheap, but the return on investment comes in less than six months from reduced downtime and scrap.
Then there’s the often-overlooked binding system for the microduct bundle. The binding unit is what holds all the individual microducts together into a single COD pipe. If the binding tension is too tight, the PE duct walls can stretch, leading to cracks or a brittle pipe that fails pressure testing. If the tension is too loose, the bundle comes apart during handling, which is a major quality defect. Many machines use old, analog tension controllers that drift over time, so the tension that was perfect at shift start is off by the end of the shift. The solution here is switching to digital tension sensors for the binding unit. These sensors adjust tension in real time based on the thickness of the PE duct, maintaining consistent tension across the entire bundle. A utility contractor I worked with had 5% of their COD pipes rejected annually because of binding issues; after installing digital tension sensors, that number dropped to 0.2%, which saved them over $40,000 a year in scrap and rework. It’s also worth noting that the binding thread itself matters—using a UV-stabilized polyester thread instead of nylon reduces breakage during production by 30%, because nylon stretches in the hot environment around the extruder, while polyester maintains its tension.
Preventive maintenance is not a chore—it’s the single biggest factor in reducing unplanned downtime. Too many plants follow a “run it until it breaks” maintenance schedule for their COD pipe machines, which means a minor seal leak turns into a full extruder failure, taking the line down for 8 hours or more. I’ve seen clients implement a simple weekly maintenance checklist that takes 2 hours to complete, and cut unplanned downtime by 40% in just three months. The checklist includes: lubricating the take-up unit’s rollers, replacing worn drive belts on the binder, checking the cooling trough’s water temperature (it should stay between 60°F and 70°F—too warm slows cooling, too cold causes thermal shock and cracking), and cleaning the extruder’s screen changer every two weeks. The screen changer is especially important: a clogged screen means the extruder has to work harder to push molten PE through, reducing line speed and putting unnecessary strain on the motor. I recommend using a hydraulic screen changer that can be swapped while the line is running, instead of a manual one that requires a full shutdown. That small upgrade alone can add 2 to 3 hours of production time per week, which adds up to 100 to 150 extra meters of COD pipe—enough to fulfill a small additional order every week.
Operator training is the final piece of the puzzle, and it’s the one that most plants neglect. I’ve seen operators with 10 years of experience run a machine at 50% of its capacity because they were taught to “keep it slow to avoid mistakes,” while a newer operator who received proper training runs it at 75% without quality issues. The key here is training that’s specific to COD pipe machines, not generic extrusion training. That means teaching operators how to adjust the extruder temperature zones based on resin type, how to interpret the line audit data to spot bottlenecks, and how to perform basic maintenance tasks like calibrating the calibrator. One client invested in a 2-day on-site training session for their operators, and within a month, their line speed increased by 17% with no drop in quality. It’s also helpful to have a cross-functional team: operators, maintenance technicians, and plant managers working together to identify issues. The operator is the one on the floor every day, so they’ll notice a small vibration in the take-up unit before it turns into a jam, and the maintenance team can fix it before it causes downtime.
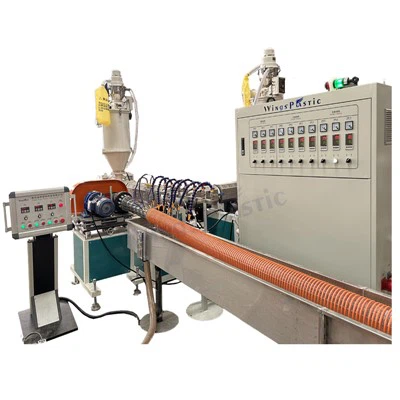
I want to be clear: none of these changes require replacing your entire machine. The average COD pipe machine has a lifespan of 15 to 20 years when maintained properly, and most efficiency gains come from small, incremental adjustments, not new equipment. I’ve worked with plants that increased their annual production by 25% without adding a single new shift, just by implementing the steps I’ve outlined here. If you’re ready to take the next step to improve your machine’s efficiency, or you have specific questions about your current setup, we’re here to help. Our team works with operators and plant managers every day to tailor solutions to their unique production needs, whether that’s upgrading a component, refining a maintenance schedule, or providing targeted training. Don’t let avoidable downtime or scrap eat into your profits—reach out to discuss how we can support your COD pipe production goals.
PVC Hose Machine References:
- Kraus, A. (2019). Extrusion Processes for Polymer Pipes and Profiles. Hanser Gardner Publications.
- Telecom Infrastructure Alliance. (2021). Best Practices for Microduct Bundle Pipe Production. TIA Technical Report 100-D-007.
- Smith, L. et al. (2022). Energy Efficiency in Plastic Extrusion: A Plant-Wide Analysis. Journal of Manufacturing Processes, Vol. 78, pp. 412-425.
- International Organization for Standardization. (2020). ISO 11922:2020, Thermoplastic pipes for telecommunications and optical fiber cables – Dimensions and specifications.
Qingdao Wings Plastic Technology Co., Ltd.
As one of the most experienced pe microduct bundle pipe cod pipe machine manufacturers and suppliers in China, we also support customized service. Please feel free to buy durable pe microduct bundle pipe cod pipe machine made in China here from our factory. For price consultation, contact us.
Address: C02 Of Anshengyi Road, No.2 Fuan Industry Zone,Jiaodong Town, Jiaozhou City, Qingdao City, Shandong Province,China
E-mail: kelly@wingsplastic.com
WebSite: https://www.wingsextruder.com/
