Hey there, let’s cut to the chase—if you’re in metal fabrication, you know how frustrating a warped metal sheet is after a shear cut. You spent hours prepping materials, dialed in your machine, and boom—one side’s bent, or it’s off by a fraction that makes your whole part useless. As a metal shear supplier, I’ve heard every headache from fabricators: “My 10-gauge steel keeps warping on the 6th cut,” “I can’t get consistent straight edges without distortion,” and worst of all, “I wasted a whole sheet of stainless steel because of this garbage.” Metal Shear
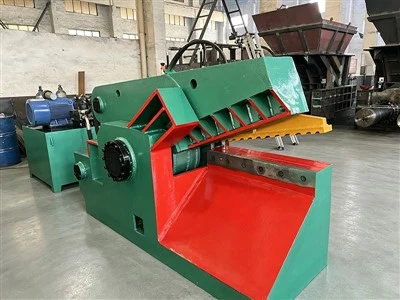
Look, distortion isn’t some mystery that only happens to “bad” operators—it’s fixable, even if you’re running a budget shear instead of a $100k industrial workhorse. I’ve been around shears for 12 years now, helping small shops and big factories alike get clean, straight cuts without that warping mess. Today, I’m spilling the exact hacks I tell every customer who calls panicking about warped sheets. Let’s dive in.
First, let’s get one thing straight: why does distortion even happen with shears? When you cut metal with a shear, you’re not just slicing through it—you’re applying force along the edge, pushing and pulling the metal as the blade pierces and shears it. That force causes internal stress in the metal sheet, especially if it’s thin (like 16-gauge or thinner) or if you’re cutting hard materials (stainless steel, aluminum alloy) that don’t give as easily as mild steel. If you don’t control that stress, the sheet twists, bows, or has that annoying “crown” (that slight curve along the cut edge) that makes fitting parts together impossible.
Most people fix distortion after it happens—they try to bend it back, hammer it flat, or run it through a press brake later. That’s a band-aid. The real win is preventing it before you even pull the shear lever. Let’s start with the basics you might be skipping, because trust me, even small, obvious steps make a huge difference.
Nail the Sheet Alignment (Seriously, Don’t Guess)
I see this all the time: a fabricator lines up a sheet, eyeballs the edge against the shear’s back gauge, and hits the pedal. That “close enough” alignment is the #1 cause of minor distortion. Why? If the sheet isn’t perfectly square to the shear’s blades, one side of the cut is taking more force than the other. That uneven force twists the sheet right there as you cut.
How to do it right? Grab a framing square (the big L-shaped one, not that tiny 6-inch thing you keep in your toolbox) and set it on the shear’s bed. Line the square’s straight edge up with the back of the shear (the stationary blade’s back stop, that bar against which you push the sheet) and adjust the back gauge until the square’s other edge is flush with the shear’s cutting blades. Wait, no—wait, you need to align the sheet’s edge to the blades, not just the back stop. Here’s the trick: for every cut, clamp a small, inexpensive straight edge (like a 2-foot steel rule) along the uncut side of the sheet, tight to the shear’s blades, to keep it from shifting mid-cut. If you’re cutting large sheets (4×8 or bigger), get two people to hold the sheet flat while you line it up—no shortcuts here. Even a 1/16th shift can add up to major distortion by the end of a cut.
Blade Tension and Gap = Make These Your BFFs
Blades on shears aren’t just sharp knives—they’re precision tools, and if they’re set wrong, distortion is inevitable. Let’s break this down: blade gap is the tiny space between the top and bottom blades. If the gap is too wide, you’re crushing the metal instead of shearing it, which creates extra stress and makes the sheet bow. Too narrow, and you’re forcing the blades through, which bends the edges and twists the sheet.
What’s the sweet spot? A general rule I’ve used for years: for every 1mm of metal thickness, set the gap to 5% of that thickness. So if you’re cutting 2mm aluminum, gap = 0.1mm. For 10-gauge mild steel (which is ~3.4mm), gap = 0.17mm. But wait—this changes if you’re cutting stainless steel. Stainless is harder, so bump the gap up to 6% to avoid work-hardening, which adds stress. Pro tip: most budget shears come with a gap adjustment gauge—use it, don’t wing it. I see customers skip this all the time, and they wonder why their cuts are warped.
Then there’s blade tension. The top blade (the moving one) has a tension screw, right? If tension is too low, the blade will wobble as it cuts, causing uneven force. Too high, and you’re putting extra stress on the blade and the sheet. How to set it? Run a piece of scrap metal the same thickness as your workpiece through the shear. If the cut edge is smooth and flat, tension is right. If it’s rough or the sheet twists mid-cut, tweak the tension screw half a turn at a time until it’s clean. Also, if your blades are dull, replace them—DULL BLADES ARE THE #1 UNDERESTIMATED CAUSE OF DISTORTION. A sharp blade slices through metal cleanly, a dull blade pushes and drags, creating all that internal stress. Don’t skimp on blade maintenance.
Clamp That Sheet Like It Owes You Money
Here’s another mistake: fabricators leave the sheet unclamped, or only clamp the ends, and wonder why the middle warps. When the shear’s blade hits the sheet, it creates a lot of downward force, especially for thin metal. If there’s nothing holding the sheet flat on the shear’s bed, it will lift, twist, or flex right as you cut.
How many clamps do you need? For small sheets (2×2), two clamps (one on each end) work. For medium sheets (4×4), four clamps—one at each corner, and one in the middle of the uncut side. For big sheets (4×8), add a clamp every 2 feet along the uncut edge. And don’t use random clamps—use the ones that came with your shear, or heavy-duty workholding clamps that are designed for shearing. C-clamps that slip or don’t press firmly enough are useless. Pro move: if you don’t have enough clamps, use weight—stack heavy plates or scrap metal on the uncut part of the sheet to hold it flat. Just make sure it’s not hanging over the bed, or you’ll get a dip in the cut.
Slow Down (Wait, Really?)
I know, I know—you’re in a rush, you have 50 sheets to cut, so you slam the pedal as hard as you can. But fast cuts = more force = more distortion. When you move the top blade too quickly, it doesn’t have time to shear the metal cleanly—it smashes it. That sudden, uneven force makes the sheet buckle.
Instead, slow down. Give the blade time to penetrate the metal gradually. For thin metal (16-gauge and up), a slow, steady cut is best. For thicker metal (10-gauge and below), you can go a little faster, but still no sprinting. I test this all the time on our shears: when I run a 16-gauge aluminum at full speed, the cut edge has a slight crown, but when I slow it down just a hair, the edge is perfectly flat. Even a 20% slower cut makes a huge difference. And one more thing—don’t cut too far. Leave a 1/8th of an inch gap at the end of the cut where the sheet meets the back gauge. If you cut all the way to the back stop, the blade will push the end of the sheet forward, causing a twist. That’s a tiny detail, but it saves so many warped sheets.
Workholding Tips for Thin or Delicate Metal
Thin metal (like 20-gauge and thinner) is a nightmare for distortion because it’s so flexible. I get it—you don’t want to clamp it so hard you leave marks, but you have to hold it flat. Here’s a trick I learned from a fabricator customer years ago: sandwich the thin sheet between two pieces of thick, flat mild steel before you cut. The bottom plate sits on the shear’s bed, the top plate has cutouts where you need to slice, and you clamp both plates together. That way, the thin metal can’t flex, and the force of the shear is spread evenly across both plates, so no distortion. After you cut, you just have a few small marks on the thick plates—easy to sand out, way better than wasting a $50 sheet of thin stainless.
Another thin metal hack: don’t cut multiple thin sheets stacked on top of each other. I see this all the time—guys stack 5 sheets of 20-gauge to cut them in one go, thinking it saves time. But each sheet flexes a different amount, so when you shear them, each warps differently, and you end up with 5 warped sheets instead of one. Cut one at a time, or stack max 2 sheets if you’re in a pinch.
Material-Specific Fixes
Not all metal is created equal. Mild steel is forgiving, but stainless, aluminum, and alloy steels are way more prone to distortion because they have higher tensile strength and work-harden easily. For stainless steel, the blade gap needs to be a little wider (like 6-7% of thickness, not 5%) to avoid work-hardening. And never use a dull blade on stainless—you’ll have to apply way more force, which causes massive stress. For aluminum, it’s soft, so make sure your clamps aren’t too tight—aluminum marks easily, but if they’re too loose, the sheet shifts. For alloy steels (like tool steel), use a slower cut and a wider gap to prevent cracking and distortion.
Common Mistakes I See All the Time (And How to Fix Them)
Let’s wrap up with the little stuff that trips people up:
- Cutting too close to the edge. If your sheet is small, and you’re cutting a piece right up to the edge of the sheet, the remaining edge is unsupported, so it warps. Leave at least 1 inch of material on each side of the cut for support, especially for thin sheets.
- Not cooling blades between cuts. If you’re cutting a lot of metal, blades get hot, which expands them. Hot blades = uneven cutting force = distortion. Wipe blades with a light oil every 10-15 cuts to cool them and prevent buildup.
- Using the wrong shear for the job. If you’re cutting 1/4-inch stainless, don’t use a 16-gauge shear. Your shear’s capacity is the maximum thickness it can cut without distortion. Using an underrated shear means you’re applying way too much force, leading to warping. It’s worth buying a shear that’s a little bigger than your current needs—trust me, the extra $500 is way cheaper than wasting materials.
Now, here’s the thing: I’m a metal shear supplier, not a magician. These steps work because they address the root cause of distortion—uneven force and internal stress in the metal. I’ve watched customers apply these hacks and cut 50 sheets without a single warp, when before they were wasting 10 sheets a week. If you’re still dealing with distortion after trying these, maybe your shear needs a tune-up, or you’re using blades that aren’t right for your material.
If you’re ready to stop wasting metal and get clean, consistent shear cuts, let’s chat. Whether you’re a small shop with a budget shear or a big factory needing industrial workholding solutions, I can help you figure out what’s causing your distortion and get you set up right. No pushy sales talk, just real advice from someone who’s been in the metal fabrication game for years. Pick up the phone and reach out, let’s find a solution that works for you.
Waste Tire Baler References:
- Kalpakjian, S., & Schmid, S. R. (2019). Manufacturing Processes for Engineering Materials (7th ed.). Pearson.
- Metal Working Machinery Association. (2021). Best Practices for Shear Operation and Maintenance.
- The Fabricator Magazine. (2022). “Reducing Sheet Metal Distortion During Shearing: A Step-by-Step Guide.”
Jiangyin Hangli Technology Co., Ltd.
Jiangyin Hangli Technology Co., Ltd. is one of the most professional metal shear manufacturers and suppliers in China. We are committed to providing high quality custom service and OEM service with low price. We warmly welcome you to buy high-performance metal shear for sale here from our factory. Also, pricelist is available.
Address: No. 11, Louxia Road, Zhouxi Village, Zhouzhuang Town, Jiangyin City, Wuxi City, Jiangsu Province, China
E-mail: sherry@hanglimachinery.com
WebSite: https://www.hanglirecycling.com/
