Hey everyone, it’s Javi here – I run the team at [Portable Milling] (our portable milling machine supplier, for anyone new here) and this week I’ve gotten so many DMs asking one specific question: “Can your portable milling machine actually mill zinc alloys?” Portable Milling

First off, let’s get this out of the way right away: YES, it can. But I’ve also seen so much misinformation online about milling zinc – like people saying it’s “too soft for portable machines” or “it’s a chip-everywhere mess that ruins tools.” Let’s break this down like we’re chatting over a coffee (no boring engineer jargon, promise) because this matters so much if you’re a fabricator, maintenance tech, or metal shop owner juggling on-site jobs, not just workbench stuff.
Wait, quick context for anyone who doesn’t deal with zinc daily: Zinc alloys aren’t just those random metal doorknobs. They’re in everything – corrosion-resistant fasteners, automotive parts (like brake caliper brackets), electrical components (terminals for wiring), even some marine hardware because zinc holds up way better to saltwater than, say, plain steel. A lot of these parts need precision milling to get their grooves, holes, or custom shapes right – and if you’ve ever had to move a 500lb part to a fixed mill, or you’re fixing something on-site (like a broken valve housing that won’t come off a pipe), you know how big of a deal portable milling is.
Now, let’s talk about why zinc feels like a tricky material for some people. First, it’s way softer than steel or aluminum – most zinc alloys have a hardness of 80–120 Brinell, vs. mild steel at ~150–200. Wait, softer sounds better, right? Well, kind of – but soft metals “gum up” tooling way easier. If you’re using a dull end mill on zinc, it’ll smear instead of cutting, leaving a rough, sticky surface that’s a nightmare to clean. Some cheap portable machines also have wobbly spindles that make the tool chatter, especially on thin zinc parts – that chatter leaves those ugly lines, and can even cause the zinc to “tear” instead of slicing clean. I’ve had a few fabricators come to me saying they burned through 3 end mills in an hour milling zinc on a off-brand portable machine – that’s why picking the right rig matters, not just “can it cut metal.”
Here’s where our portable milling machines shine, and why zinc is actually one of our most requested materials lately. First, our machines have what we call a “balanced rigid spindle” – it’s not the super high-RPM thing you see on fixed mills, but it’s built to run smooth even when cutting soft, gummy metals without chattering. We crank the spindle speed just right for zinc – around 1,200–1,500 RPM, which sounds slow for aluminum, but perfect for making zinc cut clean without gumming up. We also teach every customer (new or old) a quick trick: use up-cut end mills with a 2 flute design, not 4. More flutes mean more friction, which makes the zinc stick. 2 flutes let the chips evacuate fast, so you don’t get that messy smear.
Wait, let’s get real with a actual example – last month we worked with a shipyard in the Gulf Coast. They had to mill custom zinc alloy flanges for new marine pipe systems, and their fixed mill was booked solid for 2 weeks. One of their lead techs, Mike, rented our portable milling machine to do the job on-site at the dock. He was skeptical at first – “I’ve seen portable mills chew through brass, but zinc?” – but he texted me an hour later saying it cut through the zinc flange’s mounting holes like butter. He even added that when he used a coolant mist (not flood coolant, which is overkill for thin zinc), the parts came out so smooth he didn’t even need to sand them. That’s the real stuff, not marketing hype.
But hold on – it’s not just the machine. I can’t stress this enough: if you do it wrong, even a high-end portable mill will mess up zinc. Let’s go through the common mistakes we see, and how to avoid them. First, don’t go too deep on each pass. Zinc is soft, so it’s tempting to take big cuts to get done fast, but that’ll pull the tool out of alignment and cause that tearing we talked about. Our go-to pass depth for zinc is 0.10–0.15 inches max – that’s enough to be efficient, not enough to make a mess. Second, lubrication. You don’t need expensive synthetic coolant for zinc – even a simple water-miscible oil spray works, or even WD-40 as a quick fix for small jobs. Skip heavy flood coolant, though – zinc is prone to corrosion if it sits wet, which is a big no-no for parts that are supposed to hold up outdoors. Third, workholding. Zinc is lightweight, so if you’re milling a small part on a portable vise, clamp it tight – we recommend using low-torque clamps that don’t leave marks, or even double-sided tape for tiny bits, so you don’t shift the part mid-cut.
Another question I get: can we mill zinc alloys that are used for casting, like Zamak? For anyone who doesn’t know, Zamak is a super common zinc alloy for die-casting, used in everything from phone frames to toy parts. Yeah, that’s our bread and butter. Last quarter we had a consumer electronics company come to us – they had a batch of Zamak phone brackets that needed custom slots cut, and their die-casting tool had a broken part. They used our portable mill in their back workshop, and knocked out 200 parts in half a day. They said the finish was better than their fixed mill’s on the same job. Why? Because fixed mills for high-volume jobs can get run hard, but our portable machines are calibrated for precise, on-demand cuts – no warm-up time, no shifting the heavy part across the shop floor.
Wait, let’s address the elephant in the room: tool wear. I know someone’s gonna say “but zinc is so soft, won’t that wear tools fast?” No, not if you’re using the right setup. We use high-speed steel (HSS) end mills for most zinc jobs – they’re cheaper than carbide, and since we don’t run super high RPM, they last way longer than they would on harder metals. A good set of 2-flute HSS end mills can cut through 50+ linear inches of zinc before they need sharpening, which is way more than you’ll need for most portable jobs. And if you do use carbide (for extra-hard zinc alloys, like those with small amounts of copper or aluminum mixed in), they last even longer – we had a farmer use the same carbide end mill for 3 days milling zinc gate hinges, no issues.
I also wanna talk about when a portable mill is not the best for zinc, just to be transparent. If you need precision to within 0.001 inches for a medical-grade zinc implant, yeah, a fixed CNC mill will be better – but for 99% of the jobs our customers do, that’s overkill. If you’re working on very thin zinc sheets (under 0.05 inches) for custom craft parts, our portable mill can handle it, but you’ll need to use a slower RPM (800–1,000) to avoid bending the sheet. And if you’re doing high-volume production (like 10,000+ parts a week), a fixed mill is more efficient – but if you’re running 10, 50, or 100 parts on-site, portable is a game-changer.
Let’s wrap this up with a quick recap, because I know this is a lot: 1) Yes, portable milling machines can absolutely mill zinc alloys – we do it every single week. 2) The key is the right tool (2-flute up-cut HSS or carbide), correct RPM (1,200–1,500), shallow passes, and proper lubrication. 3) You don’t need a fancy fixed mill to get a clean, precise cut on zinc – our portable rigs are built for exactly this kind of on-demand, versatile work.
If you’re curious about how our portable mills would work for your specific zinc job – whether it’s marine parts, automotive brackets, custom hardware, or whatever else you’ve got – don’t hesitate to reach out to our team. We do free quick assessments of your project, share setup tips, and even have discounted end mill bundles for zinc cutting. No sales pitch, no pressure, just real advice from people who mill metal every day (and get frustrated by the same mistakes you do).
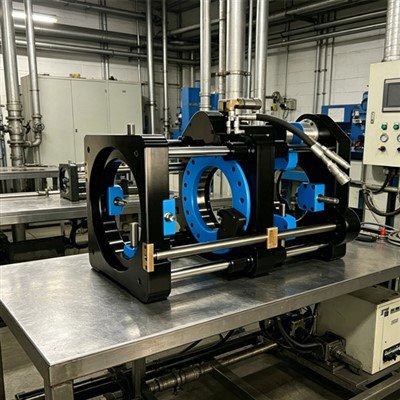
Catch you next week – until then, keep those cutters sharp!
Flange Facer References:
- ASTM International. (2020). Standard Specification for Zinc Alloy Die Castings and Zinc Alloy Ingots. ASTM B240-20.
- Machining Data Handbook. (2018). 5th Edition. Manufacturing Engineering Publications.
- National Association of Metal Formers. (2021). Portable Machining Best Practices for Soft Non-Ferrous Alloys. Industry Guide 12-21.
Shangqiu JDA Machinery Technology Co., Ltd.
With abundant experience, we are one of the most professional portable milling manufacturers and suppliers in China. We warmly welcome you to buy cheap portable milling for sale here from our factory. Quality products and reasonable price are available.
Address: No. 55 Pingyuan Middle Road, Liangyuan District, Shangqiu, Henan, China
E-mail: sales@jdamachines.com
WebSite: https://www.jdamachines.com/
