If you’ve ever ordered custom flour or grits from a specialty grocery store, you’ve used a product that passed through a plansifter—an industrial workhorse that sorts granular materials by size with precision, consistency, and far higher throughput than manual screening methods. As someone who’s spent 18 years engineering, selling, and servicing plansifters for food processing facilities, I can tell you the most common question I get from plant managers and process engineers isn’t “Does this machine work?” It’s “How do I actually calculate its sieving capacity, so I don’t buy a unit that’s too small or waste money on one that’s overkill?” Plansifter
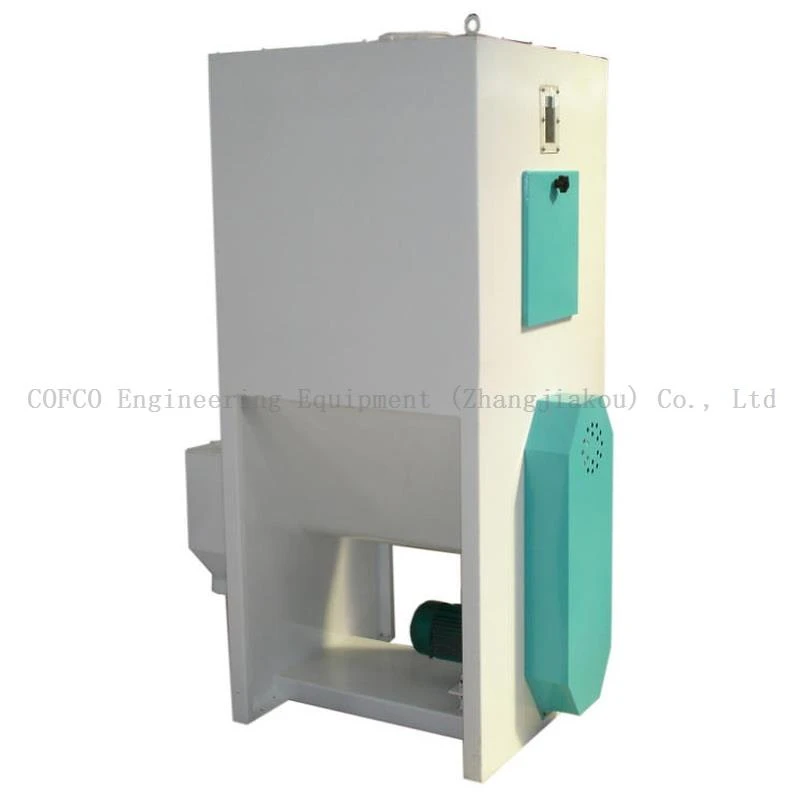
Calculating sieving capacity isn’t as simple as picking a number off a spec sheet or guessing based on the size of the machine. It’s a mix of science, experience, and an understanding of your specific product, processing goals, and facility constraints. Over the years, I’ve walked more than 200 processing plants through this process—from small specialty bakeries producing 5 tons of flour a day to large milling operations pushing 2,000 tons daily—and I’ve learned that skipping even one small step here leads to headaches down the line: bottlenecks, off-spec products, or machines that sit idle half the day. Let’s break this down step by step, using real-world examples and the data we actually rely on here at my shop.
First, let’s define what “sieving capacity” actually means in the context of a plansifter, because a lot of manufacturers will throw around terms like “throughput” or “screening rate” interchangeably, and that’s where confusion starts. For our purposes, sieving capacity is the maximum volume or mass of your granular material that a plansifter can process in a given time while meeting your product’s required sieve cut specification. A sieve cut is just the range of particle sizes you want to retain or pass through a given mesh layer. For example, if you’re producing all-purpose flour, you might specify that 98% of the material passes through a 150-mesh sieve and 2% is retained (that’s your “oversize,” which is usually bran or germ). For corn grits, you might want a uniform size, so your cut is that all grits pass through a 20-mesh sieve and are retained on a 30-mesh, with less than 0.5% of material falling outside that range.
That baseline definition is critical because it means capacity isn’t just how fast the machine runs—it’s how well it runs to your exact requirements. I once had a customer who bought a plansifter from a discount supplier because it had a larger footprint than our models, only to find out that its spec sheet “capacity” was based on processing sand, not flour. Sand has very uniform, round particles that pass through sieves much faster than flour, which is irregular and absorbent. By the time they realized that unit could only process half the flour they needed, they’d wasted six weeks of downtime and rework.
Now, let’s get into the actual calculations. There are five core factors we use to determine a plansifter’s sieving capacity, and each one is weighted based on your specific application. I’ll walk you through each with concrete numbers, using common food processing products as examples, so you can follow along.
First factor: Particle size and shape of your feed material. This is the most variable, and the one that trips up the most first-time users. The rate at which material passes through a sieve (called “passing rate”) depends directly on how close each particle is to the sieve’s opening size. If you’re working with flour that’s 150-mesh (meaning most particles are 100 microns, and the sieve openings are 105 microns), almost every particle that hits the sieve will pass through. If your feed is wheat that has 20% oversize bran particles of 300 microns, only a small fraction will fit through the 150-mesh openings. Particles also matter: round, uniform grains (like rice) roll through sieves and pass much faster than irregular, jagged particles (like whole wheat flour, which has sharp bran flakes that get stuck in mesh). To account for this, we use a number called the “particle shape factor,” which ranges from 0.6 for irregular particles to 0.95 for spherical grains. For most flours, we use 0.7; for corn grits, it’s 0.85; for bran, it’s 0.5.
Second factor: Total effective sieve area. This is where a lot of marketing hype comes in. Spec sheets will list a plansifter’s “total screen area” as something like 12 square meters, but that’s not the number you care about. What matters is effective sieve area—the portion of the total screen that’s actually usable for sieving, not blocked by frames, dividers, or the feed entry point. For a standard plansifter, effective area is usually 70-80% of the total listed area, depending on the number of sieve layers. For example, a 10-layer plansifter with 1.5 square meters per layer has a total screen area of 15 square meters, but effective area is 12 square meters (80%) after accounting for dividers and crossbars. This is why two plansifters with the same total footprint can have very different actual sieving capacity—one might have thicker frame dividers that waste screen area, while our designs have thin, precision-machined dividers that maximize usable space.
Third factor: Vibration characteristics of the plansifter. Plansifters rely on controlled horizontal vibration to move material across the screens, prevent clogging, and get particles to bounce into the sieve openings. If vibration is too weak, material pools on the screens and doesn’t move through; if it’s too strong, particles bounce right off the sieve, leading to oversize in your final product. The right vibration is specific to your material and sieve size. For flour, we typically set vibration at 8-12 mm amplitude at 500-600 RPM; for larger particles like grits, it’s 10-15 mm amplitude at 400-500 RPM. This affects capacity because optimal vibration reduces the time particles take to pass through the screens. Our plansifters use balanced eccentric motors that deliver consistent, adjustable vibration across all sieve layers, so capacity remains stable even during long runs. A common mistake here is users who crank up vibration to speed up processing, which actually leads to more oversize particles and off-spec product—lowering effective capacity by 15-20%.
Fourth factor: Moisture content of your feed. This is a deceptively simple factor that has a huge impact on sieving capacity. If your material is too dry, it’s prone to dusting, which gets sucked out of the plansifter by the machine’s ventilation system—meaning you lose product and reduce overall throughput. If it’s too moist, particles clump together, sticking to each other and clogging sieve openings, so almost no material passes through. For most grain products, the ideal moisture content for optimal sieving is 12-14% for flour, 14-16% for corn grits, and 10-12% for rice. I once had a customer process flour that was 8% moisture because they’d dried it too much for a baking application, and their sieving capacity dropped by 40%—the fine flour dust was being pulled out of the machine’s exhaust, and clumps of flour clogged every 150-mesh screen layer every 2 hours. They fixed it by adjusting their drying process to get to 12% moisture, and capacity went right back up.
Fifth factor: Target sieve cut precision. Last, and often overlooked, is how precise you need your final cut to be. If you’re making animal feed, where a cut that’s off by 5% is acceptable, you can push the plansifter to maximum capacity because you don’t have to waste time or material separating the slightly off-spec particles. But if you’re making premium cake flour, where you need 99.5% of particles between 100 and 150 microns, you have to run the plansifter at a lower throughput to get that precision. For premium products, capacity is typically 60-70% of the maximum theoretical capacity; for bulk products like animal feed, it can be up to 90%.
Putting all these factors together, the basic formula for sieving capacity (in kg/hour) is:
Sieving Capacity = (Effective Sieve Area × Passing Rate × Particle Shape Factor × 60 minutes) × (1 – Target Precision Buffer)
Wait, let’s make that concrete so you can plug numbers in. Let’s use an example: a specialty bakery producing premium all-purpose flour, which needs a 150-mesh cut, 12% moisture flour (particle shape factor = 0.7, passing rate = 0.85, target precision = 98%, so buffer = 0.3). The plansifter has 12 square meters of effective sieve area.
Calculation:
12 m² × 0.85 passing rate × 0.7 shape factor × 60 minutes × (1 – 0.3) = 12 × 0.85 = 10.2; 10.2 × 0.7 = 7.14; 7.14 × 60 = 428.4; 428.4 × 0.7 = ~300 kg/hour. That means this plansifter will process about 300 kg of premium all-purpose flour per hour while meeting their precision requirement. If that same bakery was making bulk animal feed, with a precision buffer of 0.1, capacity jumps to ~450 kg/hour.
But here’s the thing: this formula is a baseline. Every application has unique quirks, so the formula is just a starting point. That’s why our team always recommends running a sample test of your product on our demonstration plansifters before committing to a purchase. We have a 1,200-square-foot test facility where we host customers from all over the world, and we can simulate their exact feed, moisture, and precision requirements to get an accurate capacity number, no guesswork needed.
I’ve seen too many companies skip this test and order the wrong size plansifter. A grain mill in Kansas once ordered three 500 kg/hour plansifters, based on a generic formula for wheat flour, only to find that their specific hard red wheat had a higher bran content, lower passing rate, so each unit could only do 350 kg/hour. They had to shut down one of their milling lines for two weeks to reconfigure, costing them over $100,000 in lost production. A quick test on our demo unit would have caught that discrepancy before they placed their order.
Another key consideration when calculating sieving capacity is the lifespan of the sieves themselves. As screens get clogged over time, the effective area drops by 5-10% after 6 months of use, so you need to build a buffer into your initial capacity calculation to account for that. We sell our customers replacement sieve sets at a 30-day discounted rate, because we know proper maintenance keeps capacity consistent long-term.
Now, let’s talk about common pitfalls that skew capacity calculations, that I see every day:
- Confusing total screen area with effective area: As I mentioned earlier, spec sheets will brag about big total areas, but if half that area is blocked by frames, it’s useless. Always ask for the effective screen area, not just the total.
- Using generic passing rates: Most manuals give a passing rate for round, uniform particles, but your product is almost never that. For example, whole wheat flour has a passing rate 20% lower than refined all-purpose flour, because of the jagged bran particles.
- Ignoring moisture content: Even a 2% difference in moisture can change capacity by 10-15%, as clumping or dusting starts. We always ask for your actual feed moisture, not the rated value from your raw material supplier.
- Underestimating maintenance time: If your production line runs 24/7, you need to schedule 15 minutes every 8 hours to clean screens, which means the effective operating time of the plansifter is not 24 hours, it’s ~22.5 hours. Factor that into your total daily capacity.
At the end of the day, calculating a plansifter’s sieving capacity is less about math and more about understanding your own process needs, and partnering with a supplier who knows how to translate those needs into accurate, real-world numbers. I’ve been doing this long enough that I can look at a customer’s product sample, their daily production goals, and give them a rough capacity estimate in 10 minutes, but I always back that up with a test run.
If you’re in the market for a plansifter and need an accurate sieving capacity calculation, or if you’re troubleshooting underperformance on your current unit, we’re here to help. We’ve worked with small craft bakeries, large milling operations, and everything in between, and we pride ourselves on giving honest, data-driven advice—not overinflating numbers to make a sale. We can walk you through the step-by-step calculation, run a test on your product, and help you pick the right size plansifter that meets your throughput and quality requirements, no guesswork needed. Reach out to discuss your specific application today.
Feed Mixing Equipment References
- Posner, E. S., & Hibbs, A. N. (2005). Wheat Flour Milling, 2nd Edition. American Association of Cereal Chemists International.
- Jones, R. L. (2018). Industrial Screening and Sizing Equipment: Selection, Operation, and Maintenance. Elsevier.
- Milling and Grain Technology Association. (2021). Recommended Practices for Plansifters in Grain Processing. Milling and Grain Society.
- Davis, L. A. (2019). Particle Technology for Food Processing. CRC Press.
COFCO Engineering Equipment (Zhangjiakou) Co., Ltd.
As one of the most professional plansifter manufacturers and suppliers in China, we also support customized service. Please feel free to wholesale advanced plansifter for sale here from our factory. Quality products and reasonable price are available.
Address: No.4 ZhongLiang Street, high-tech industrial development zone, Zhangjiakou, Hebei, PRC
E-mail: mayihui@cofco.com
WebSite: https://www.ceeflourmill.com/
